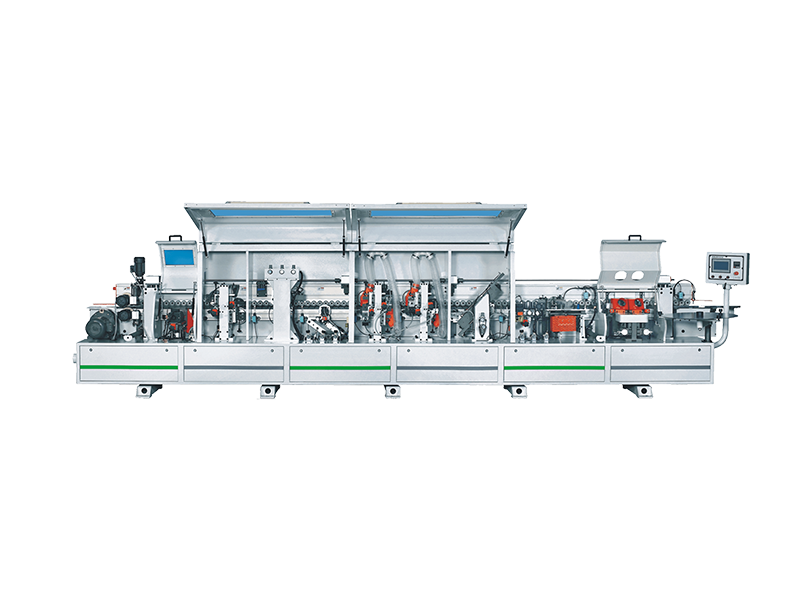
How to adjust the strength and advance of each part of the automatic edge banding machine?
1. There are two straight dispatch handles at the finishing knife. The left dispatch handle adjusts the up and down processing amount of R knife, and the right dispatch handle adjusts the up and down processing amount of R knife. (Opposite for the left feed model). Two motor tail each has a scheduling handle, separate the corresponding scheduling R knife to repair the processing amount of R. Motor tail scheduling handle clockwise rotation is R knife - sealed edge R is small, on the contrary, are in R knife - sealed edge R is large. The two need to work together, talent to bring out smooth lines, smooth R.
2. The scheduling strength, scheduling method and precautions of the press wheel are the same as the scheduling strength, methods and precautions of the press wheel at rough repair. The scheduling force of the upper and lower taper wheel is arranged by the chuck screw on the motor base. Clockwise rotation increases the pressure, and conversely, the pressure decreases. Scheduling intensity is too large, when sealing the workpiece taper wheel seat back resistance is too large, affect the trimming, and even in the process of machining the workpiece and equipment. Scheduling intensity is too small, sealing workpiece taper wheel.
3. The entry and exit of the upper and lower taper wheel are divided into two kinds: the individual entry and exit scheduling and the whole entry and exit scheduling. Separate access up and down can be carried out through the taper wheel support seat. When scheduling, first loosen the support seat scheduling fastening handle, and then move the support seat forward or backward, but it is necessary to make the two taper wheels very evenly against the workpiece, and then lock the handle tightly, otherwise it will affect the trimming. All in and out through knurled handle scheduling, counterclockwise rotation, the feed increases, otherwise, the feed decreases. Too much, easy to make the workpiece front-end harm, and even damage the equipment. Too little adjustment affects trimming. Generally, the taper wheel can be pushed back about 2mm by the workpiece, and the double-sided knife should be smaller.
4. R knife out of the workpiece is necessary to leave a small amount of sealing belt margin, for the scraper to scrape. With too much margin, the back end of the workpiece tends to appear a little without sideband. The margin is too small for the scraper to scrape the side band.
Temperature problem of automatic edge banding machine:
In the operation of the edge banding machine, temperature becomes an important reason for its operating efficiency because of its thermal melt adhesive function.
The hot melt adhesive temperature, substrate temperature, edge data temperature and operating environment (the location of the edge banding machine workshop) temperature are very important edge parameters. In the active edge banding machine because the glue is coated on the base material, the temperature is too low the base material will make the hot melt adhesive cure in advance, and then lead to the glue can stick to the base material, but it is not strong bonding material, the temperature of the base material is best to keep above 20°C.
The operating temperature of the banding machine will affect the curing speed of the glue. Factories often appear in the season of low temperature edge problems, the reason is that the low temperature of the hot melt adhesive curing speed is accelerated, the useful bonding time is shortened. If the feed rate of the edge banding machine can not be changed (in most cases), to ensure the quality of the edge must preheat the sheet and edge data.
 Fax: 0769-82682014
 Call : 138 2927 5136
 Email: dghuaweying66@163.com
 Address: Room 103, No.17, East Furniture Avenue, Houjie Town, Dongguan City, Guangdong Province
Plate type series equipment
Solid wood series equipment
Fittings for woodworking machinery
Full automatic high speed edge sealing machine
 Service hotline
138-2927-5136
If you have any questions to consult the company, you are welcome to call
 Sweep the qr code
Official Accounts